Rice bran oil manufacturing represents a sophisticated journey that begins in the rice mill and ends with a clear, stable product ready for kitchens and food industries around the world. The raw material originates from the thin brown layer that surrounds the rice grain. During milling, this layer is separated as bran, a nutrient-rich fraction containing oil, proteins, and valuable bioactive compounds. Because the bran is highly active biologically, immediate attention is required to preserve quality. Without timely handling, natural enzymes can break down the oil, affecting flavor and stability.
The first crucial step after separation is stabilization. Fresh bran contains enzymes that rapidly initiate degradation. Heat treatment halts this activity, protecting the oil from unwanted changes. Stabilization is therefore essential for maintaining the integrity of the material and enabling further processing. Once treated, the bran becomes suitable for storage and transport to extraction facilities.
Moisture management follows stabilization. Drying reduces water content to levels that favor efficient extraction and safe handling. Excess moisture can interfere with machinery performance and may encourage spoilage. Careful control ensures that the bran remains in ideal condition for the stages that follow.
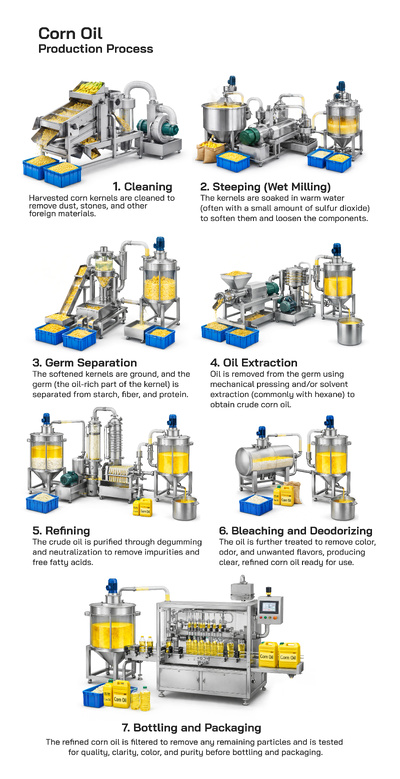
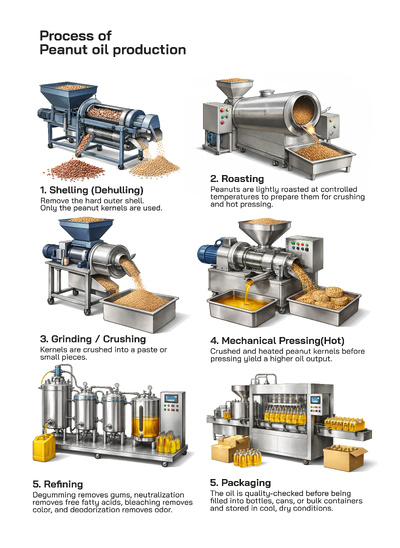
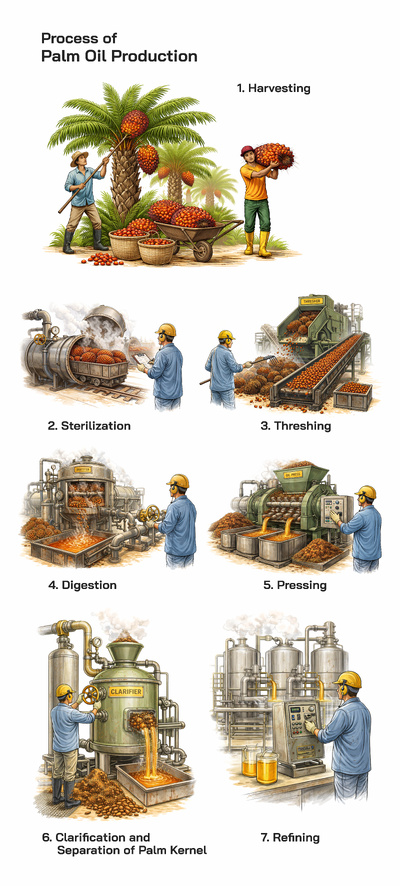
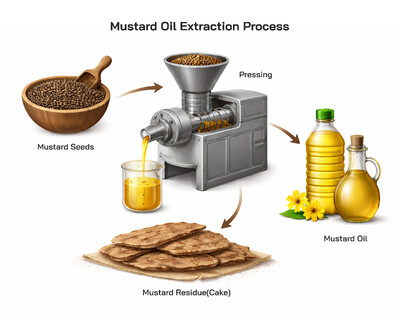
Mechanical pressing is often the initial method used to release oil. In this approach, expellers apply pressure that squeezes liquid from the solid matrix. The resulting crude oil contains not only triglycerides but also impurities such as gums, pigments, and traces of other materials. While pressing alone can recover a significant portion, additional methods are frequently employed to increase efficiency.
Solvent extraction is widely adopted to retrieve more oil from the remaining solids. A solvent dissolves the oil, enabling separation from the meal. Afterward, the mixture undergoes recovery processes to remove the solvent, leaving behind crude oil ready for refining. This stage significantly improves yield, making large-scale production economically viable.
Once crude oil is obtained, refining begins. Degumming is among the earliest steps, targeting phospholipids and gummy substances that can affect clarity and storage behavior. Removing these components improves stability and prepares the oil for subsequent purification. Neutralization follows, focusing on free fatty acids that may contribute to off-flavors or reduced shelf life. Through controlled reactions, these unwanted elements are separated from the main fraction.
Bleaching addresses color and residual impurities. Specialized materials adsorb pigments, metals, and other traces, resulting in a lighter, cleaner appearance. This transformation is not merely cosmetic; it also supports consistency and consumer acceptance. After bleaching, the oil moves to deodorization, where steam under vacuum eliminates volatile compounds responsible for odor. The outcome is a neutral aroma, essential for versatility in cooking and food manufacturing.
Winterization represents another refinement, particularly important when clarity at lower temperatures is desired. During this stage, waxes that might otherwise create cloudiness are removed. The oil becomes more transparent and visually appealing, qualities highly valued in retail markets.
Before reaching consumers, the refined oil typically undergoes final filtration. This ensures that any remaining particles are removed, leaving a smooth, stable liquid. Packaging then takes place under hygienic conditions, with containers designed to protect against light and contamination. Labels provide information, and the product enters distribution channels that may span continents.
The global importance of rice bran oil production continues to expand. As consumers seek alternatives that balance functionality with nutritional interest, this oil has gained recognition. Advances in technology allow manufacturers to recover valuable components efficiently while maintaining high standards of safety and quality.
Culturally and economically, rice bran oil demonstrates how a milling by-product can become a premium commodity. What begins as a thin layer around a grain of rice ultimately supports industries, livelihoods, and culinary traditions. This transformation highlights the power of innovation in turning residual material into something of significant value.
Rice bran oil production represents one of the most sophisticated transformations within agro-processing, linking cereal milling operations with modern refining science. Once the bran fraction becomes available, the challenge is no longer simply separating liquid from solid; instead, manufacturers must preserve fragile components, manage rapid biochemical change, and design systems capable of delivering consistent quality to diverse markets. The pathway from raw material to finished oil therefore involves an intricate choreography of engineering, chemistry, and logistics that extends far beyond the simple description of each stage.
A central concern throughout the process is time. Fresh bran is biologically active, and delays between milling and treatment can influence final performance. Facilities are often organized so that stabilization, handling, and extraction units operate in close coordination, minimizing exposure to uncontrolled conditions. Conveyors, sealed transfer systems, and automated feeders reduce human contact and help maintain traceability. This integration ensures that the valuable lipid fraction is protected from deterioration before it even reaches the refinery.
Material handling technologies contribute significantly to efficiency. Pneumatic transport, magnetic separators, and vibrating screens are employed to maintain cleanliness and protect equipment from wear. Even small contaminants can damage high-precision machinery or interfere with later purification steps. By investing in robust pre-processing safeguards, plants avoid costly interruptions and maintain predictable throughput. These preventive measures may not be visible in the final bottle, yet they underpin reliability across the entire enterprise.
Energy management forms another crucial dimension. Rice bran oil factories consume heat, electricity, and sometimes steam in large quantities. Modern installations attempt to recover energy wherever possible, capturing waste heat from one operation to support another. Insulated pipelines, optimized burner systems, and automated temperature regulation reduce losses. Such strategies not only improve economic performance but also respond to growing pressure for environmentally responsible production.
Water use must also be controlled carefully. Though essential for certain refining activities, excess consumption creates disposal challenges. Treatment facilities recycle process water, removing residues before reuse or safe release. Advanced filtration and biological treatment units allow plants to meet stringent environmental standards while minimizing freshwater demand. These investments reflect the recognition that sustainability increasingly influences market access.
Quality control laboratories operate alongside the physical plant, analyzing samples at multiple points. Technicians measure parameters such as moisture, acidity trends, color indices, and trace contaminants. Continuous monitoring allows operators to adjust conditions before deviations escalate. This scientific oversight transforms manufacturing into a dynamic system capable of responding quickly to variation in raw material supply.
Another layer of complexity involves micronutrients naturally present in rice bran oil. Components such as tocopherols and oryzanol attract interest because of their functional properties. Refiners seek to retain beneficial fractions while still achieving the clarity and stability required by consumers. Achieving this balance requires precise calibration of temperature, pressure, and contact times. Too aggressive an approach may reduce desirable elements, while insufficient treatment can compromise shelf life.
Automation has reshaped workforce roles within these facilities. Instead of manual intervention, operators supervise computerized panels that display flow rates and system diagnostics. Predictive maintenance algorithms alert staff to wear before breakdown occurs. Training therefore emphasizes technical literacy and problem-solving skills, enabling personnel to manage increasingly complex environments.
Supply chain coordination begins well before packaging. Bulk storage tanks must protect oil from oxidation and contamination while accommodating fluctuations in demand. Nitrogen blanketing, temperature monitoring, and carefully designed transfer pumps maintain integrity during holding periods. From these reservoirs, product may move to blending units where specifications are tailored for particular customers.
Market diversification has encouraged producers to create multiple grades. Cooking applications, nutritional supplements, and industrial uses may each require different attributes. Refinery managers design flexible lines capable of switching between targets without extensive downtime. This adaptability provides resilience when consumer preferences shift.
Safety protocols remain paramount throughout operations. High temperatures, flammable materials, and pressurized systems demand rigorous standards. Regular audits, emergency planning, and employee training help prevent accidents. By embedding safety culture into daily routines, companies protect both workers and investment.
Innovation continues to influence the future of rice bran oil manufacturing. Researchers investigate enzymatic treatments, membrane filtration, and improved adsorption materials that could enhance selectivity and reduce resource consumption. Pilot plants test these ideas, translating laboratory insights into scalable solutions. Progress in this area may redefine efficiency benchmarks in the coming decades.
As rice bran oil manufacturing matures, competitive advantage increasingly arises from how effectively companies integrate refinement with broader industrial ecosystems. Production plants rarely operate as isolated units; they function as hubs connected to farmers, millers, chemical suppliers, packaging firms, distributors, and retailers. Each participant influences timing, specification, and cost. Managers therefore focus on coordination mechanisms that allow information to travel rapidly across this network, ensuring that decisions made at one point do not create inefficiencies elsewhere.
Digital transformation is accelerating this integration. Enterprise software systems track incoming raw materials, monitor processing variables, and map finished goods to customer orders. With real-time dashboards, planners can forecast inventory requirements or anticipate maintenance windows. When deviations appear, corrective action can be initiated immediately, minimizing disruption. Such visibility fosters confidence among buyers who depend on uninterrupted supply.
Traceability has become especially significant in international trade. Importing countries frequently demand assurance about origin, handling, and compliance with safety norms. Manufacturers respond by building documentation frameworks that follow each batch from arrival to dispatch. Barcoding, automated sampling, and secure databases support this effort. Transparent records not only satisfy regulators but also strengthen brand reputation in increasingly competitive markets.
Another expanding frontier involves valorization of secondary outputs. During refining, various fractions separate from the primary oil stream. Instead of viewing them as waste, innovative companies identify applications in feed, pharmaceuticals, or specialty chemicals. By developing parallel product lines, they increase revenue while reducing environmental burden. Circular thinking of this kind reflects a shift toward maximizing resource efficiency throughout the facility.
Investment in human capital remains just as important as machinery. Modern plants rely on multidisciplinary teams that combine engineering expertise with analytical capability. Continuous professional development programs help employees adapt to evolving technologies. When staff understand both operational detail and strategic objectives, they contribute ideas that improve performance. Knowledge-sharing cultures can thus be powerful engines of innovation.
Public expectations regarding sustainability continue to reshape priorities. Consumers increasingly want assurance that food production aligns with environmental and social responsibility. Manufacturers respond through certifications, renewable energy adoption, and community engagement initiatives. Solar installations, biomass boilers, and waste-reduction campaigns demonstrate commitment while often lowering operating costs over time. Transparent reporting communicates these achievements to the marketplace.
Research partnerships between industry and academia deepen understanding of process optimization. Universities explore catalytic behavior, adsorption efficiency, and advanced sensor technology, while companies provide real-world testing grounds. Such collaborations shorten the distance between theory and application. Breakthroughs emerging from these alliances may deliver improved yields, reduced emissions, or enhanced nutritional retention.
Globalization introduces both opportunity and complexity. Diverse culinary traditions and regulatory standards require tailored approaches. Some markets emphasize nutritional enrichment, others prioritize long frying stability or neutral flavor. Manufacturers must therefore remain agile, adjusting specifications and packaging formats according to destination. Export strategies hinge on accurate interpretation of these preferences.
Brand development has also grown more sophisticated. Rather than selling anonymous commodity oil, companies craft narratives around quality assurance, heritage, and technological leadership. Marketing departments collaborate closely with production teams to ensure claims reflect genuine capability. Authentic storytelling becomes a differentiator in crowded retail environments.
Financial planning intersects with manufacturing decisions in significant ways. Large investments in equipment or environmental controls require long-term outlooks. Firms analyze projected demand, currency fluctuations, and trade policy before committing capital. Successful strategies balance ambition with prudence, ensuring resilience during market volatility.
Future prospects suggest continued convergence between food science and industrial engineering. As measurement tools become more precise, operators will be able to customize refining intensity with unprecedented accuracy. Adaptive systems may respond automatically to variation in incoming material, optimizing outcomes without constant supervision. Such advancements promise greater consistency while reducing resource use.
The evolution of rice bran oil manufacturing thus reflects a broader transformation in how agriculture interacts with technology and commerce. What begins as a milling by-product ultimately becomes part of a global narrative about sustainability, nutrition, and innovation. By nurturing collaboration across disciplines and borders, the industry demonstrates how complex challenges can be addressed through coordinated effort.
In this expanding landscape, success depends not only on mastering individual steps but also on harmonizing them within a responsive, transparent, and forward-looking system. The factories of today are laboratories of continuous improvement, where incremental gains accumulate into significant progress. Through dedication to excellence, rice bran oil producers continue to elevate the value derived from one of the world’s most abundant crops.
Ultimately, the industry illustrates how agricultural by-products can become high-value commodities when supported by technology and organization. From synchronized logistics to advanced analytics, every component contributes to transforming a perishable raw material into a stable, market-ready oil. Appreciating these hidden layers deepens understanding of the remarkable journey that occurs behind the scenes of everyday products.
In summary, the manufacturing pathway from bran separation to final packaging involves stabilization, extraction, purification, and finishing steps carefully designed to deliver a reliable product. Each phase contributes to clarity, flavor neutrality, and storage stability. Through this intricate process, rice bran oil moves from the mill to markets worldwide, exemplifying efficiency and ingenuity in modern food production.